High quality, Well-deserved reputation, First-class service
PRODUCTS
CONTACT INFO
Email: sales01@everluckymachinery.com
Whatsapp: +86-13722852356
Wechat: ff0082006
Sype: 297338284@qq.com
Tel: +86-317-5660915
Fax: +86-317-8330026
Address: Botou city Hebei province

Advanced Air Slide Conveyor System Featuring a Robust Industrial Powder Diverter Valve
Airslides are used extensively in conveying homogenous dry powder in many industries including minerals and mining where it is used in cement
Category
Contact Info
sales01@everluckymachinery.com
Product Details

Advanced Air Slide Conveyor System Featuring a Robust Industrial Powder Diverter Valve
Introduction
The Air Slide Conveyor System
Structure and Design
- Trough Design: The air slide conveyor's trough is engineered with precision. Its smooth interior surface is designed to minimize friction, ensuring that powders flow effortlessly. The trough is made from high - quality, wear - resistant materials, such as special alloy steels. This not only enhances the durability of the trough but also reduces the risk of material buildup, which could otherwise disrupt the flow of powder.
- Air Supply System: A crucial component of the air slide conveyor is its air supply system. It consists of high - efficiency blowers and a network of air ducts. The blowers are carefully selected to provide a consistent and controlled airflow. This precisely regulated air pressure beneath the powder layer fluidizes the powder, transforming it into a semi - fluid state for easy conveyance. The air ducts are designed with a smooth inner finish and optimized bends to minimize air resistance, ensuring that the air reaches all parts of the trough evenly.
Operational Advantages
- Gentle Material Handling: One of the key advantages of our air slide conveyor system is its ability to handle powders gently. Unlike some mechanical conveying systems that can cause particle degradation, the air - assisted flow in our system ensures that the integrity of the powder particles is maintained. This makes it ideal for conveying delicate powders, such as those in the pharmaceutical or food industries.
- High - Volume Capacity: The system is designed to handle large volumes of powder. The combination of the wide - width trough and the efficient air supply allows for high - throughput conveying. Whether it's in a large - scale chemical plant or a cement manufacturing facility, our air slide conveyor can keep up with the production demands, ensuring a continuous and smooth flow of materials.
The Robust Industrial Powder Diverter Valve
Valve Structure
- Body Construction: The diverter valve body is crafted from heavy - duty cast iron or stainless steel, depending on the application requirements. Cast iron offers excellent strength and durability, making it suitable for general industrial applications where cost - effectiveness is a priority. Stainless steel, on the other hand, provides superior corrosion resistance, making it ideal for industries dealing with corrosive powders or in harsh environmental conditions.
- Internal Components: The valve features precision - machined internal components. The sliding gate or the rotating disc (depending on the valve type) is designed to provide a tight seal when in the closed position. This prevents powder leakage, ensuring efficient material distribution. The components are made from hardened materials to withstand the abrasive nature of powders during operation.
Operational Features
- Precise Diverting: The powder diverter valve allows for precise control over the flow of powder. With its easy - to - operate manual or automated control mechanisms, operators can quickly and accurately direct the powder to different destinations. This is essential in industries where multiple processing lines or storage silos need to be fed with the correct amount of powder at the right time.
- Versatility: Our diverter valve can handle a wide range of powder types, from fine, dusty powders to coarser granular materials. It can be configured to operate in various orientations, providing flexibility in system integration. Whether it's a horizontal, vertical, or angled installation, the valve can be adjusted to suit the specific layout of the powder handling system.
Factory Design and Quality Advantages
Design Advantages
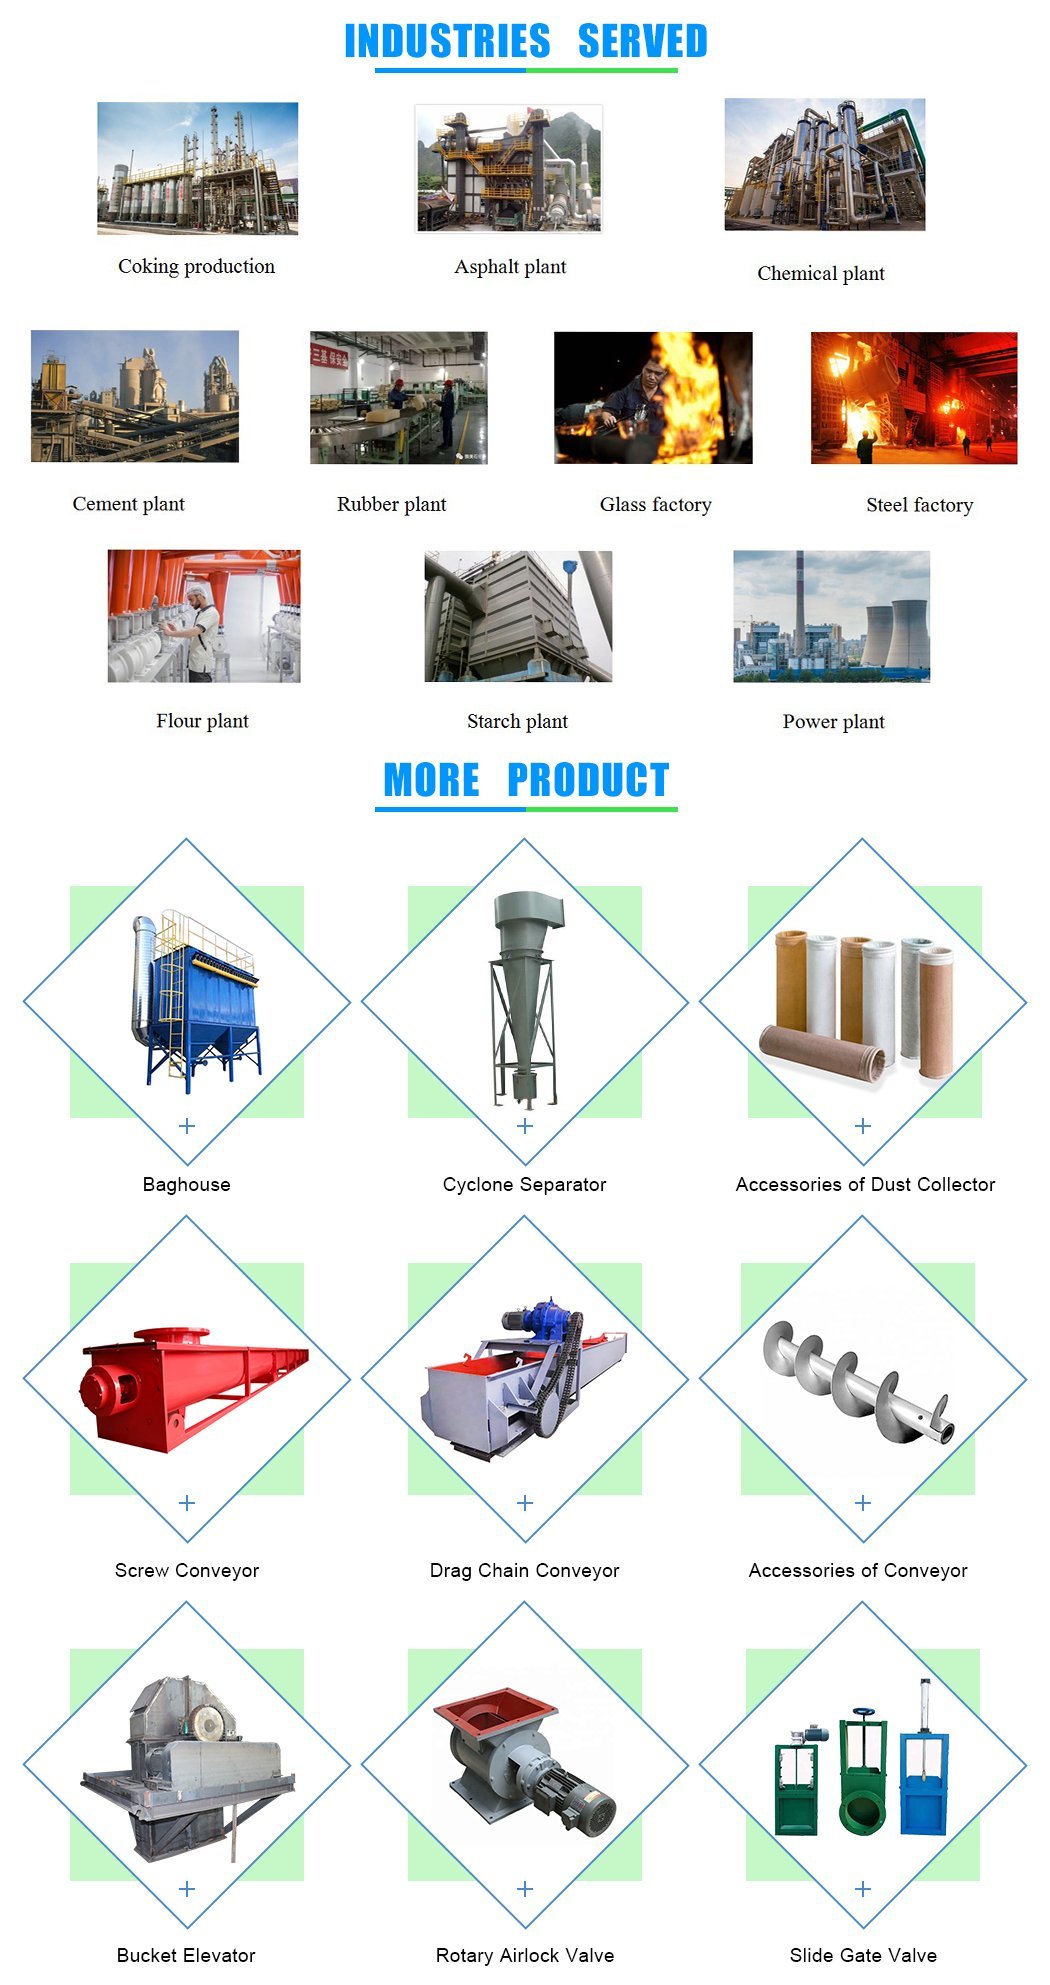
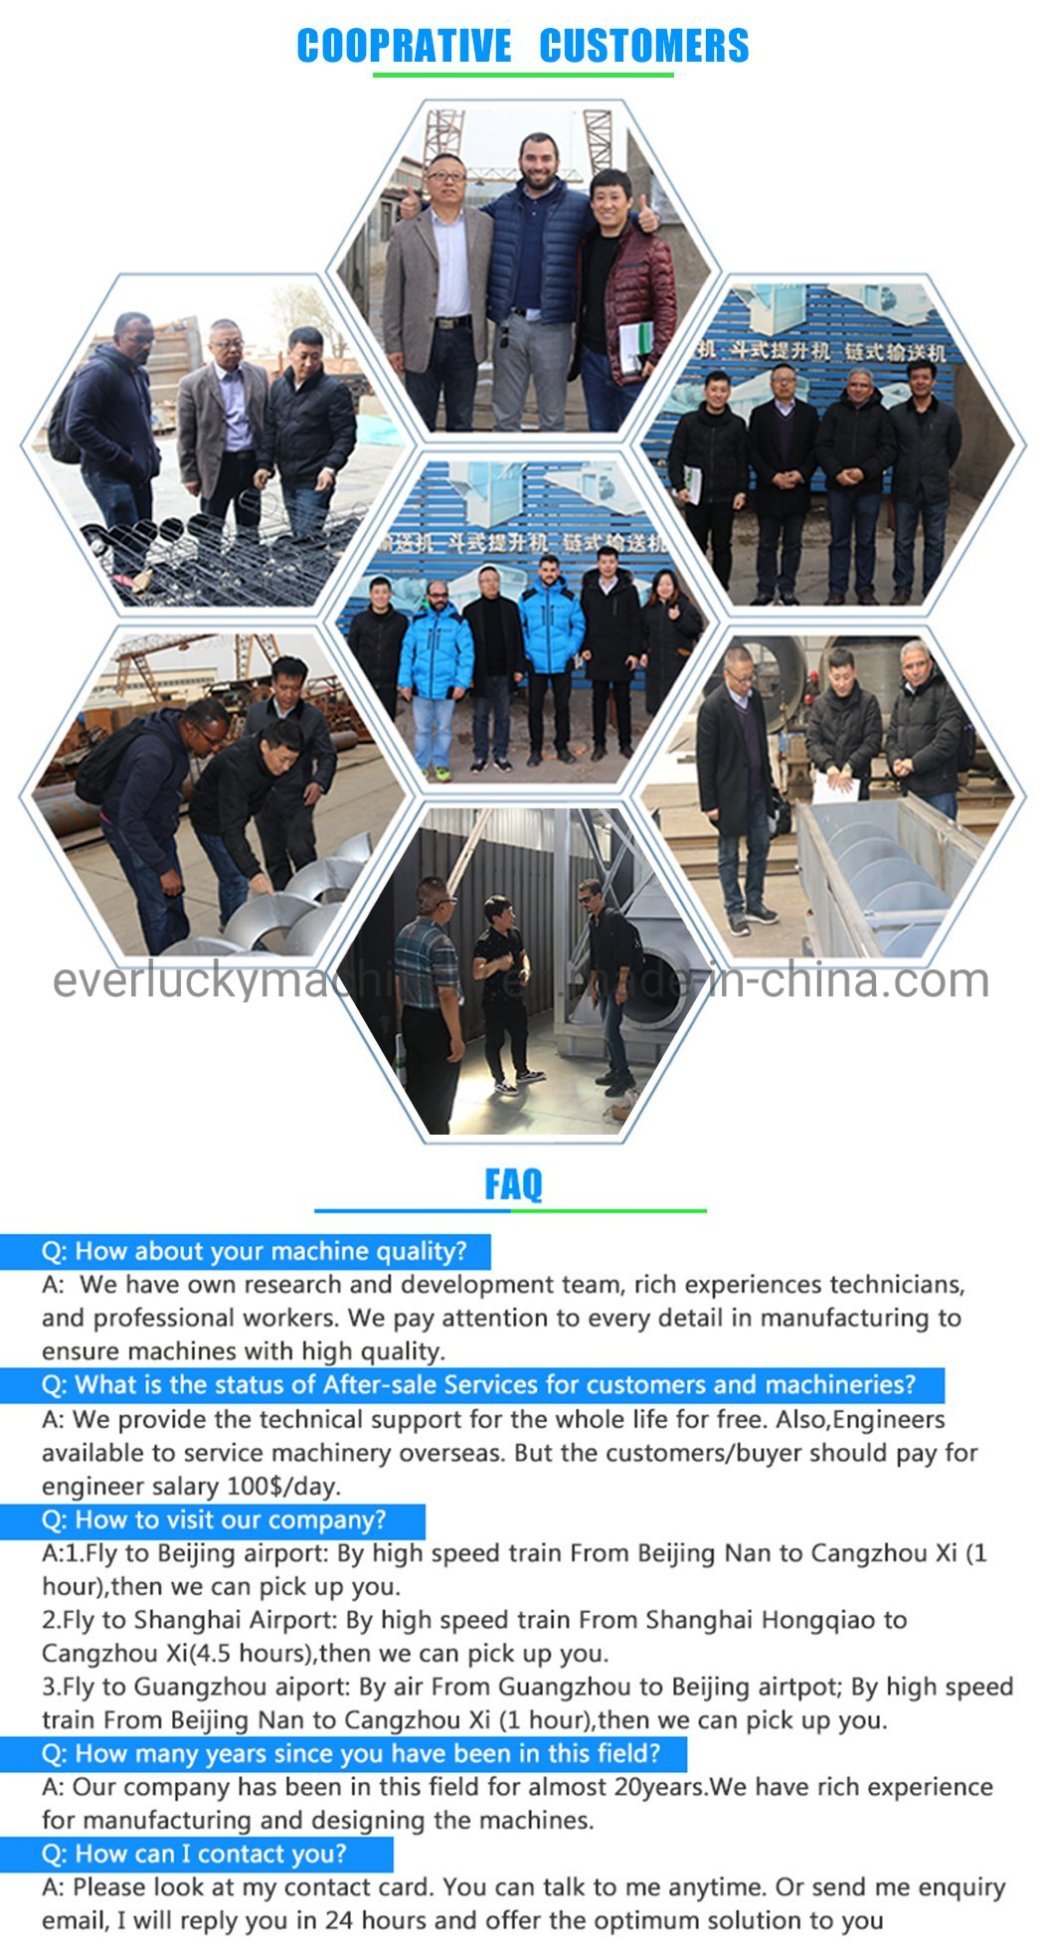
- Custom - Tailored Solutions: Our factory's engineering team works closely with customers to understand their specific powder handling needs. We offer custom - designed air slide conveyor systems and diverter valves to ensure that each installation is optimized for the client's processes. This includes considerations such as the type of powder, throughput requirements, available space, and integration with existing equipment.
- 3D Modeling and Simulation: During the design phase, we utilize advanced 3D modeling and simulation software. This allows us to visualize the system's operation, identify potential issues, and optimize the design before production. By simulating the flow of powder and air within the system, we can fine - tune the design to achieve maximum efficiency and reliability.
Quality Advantages
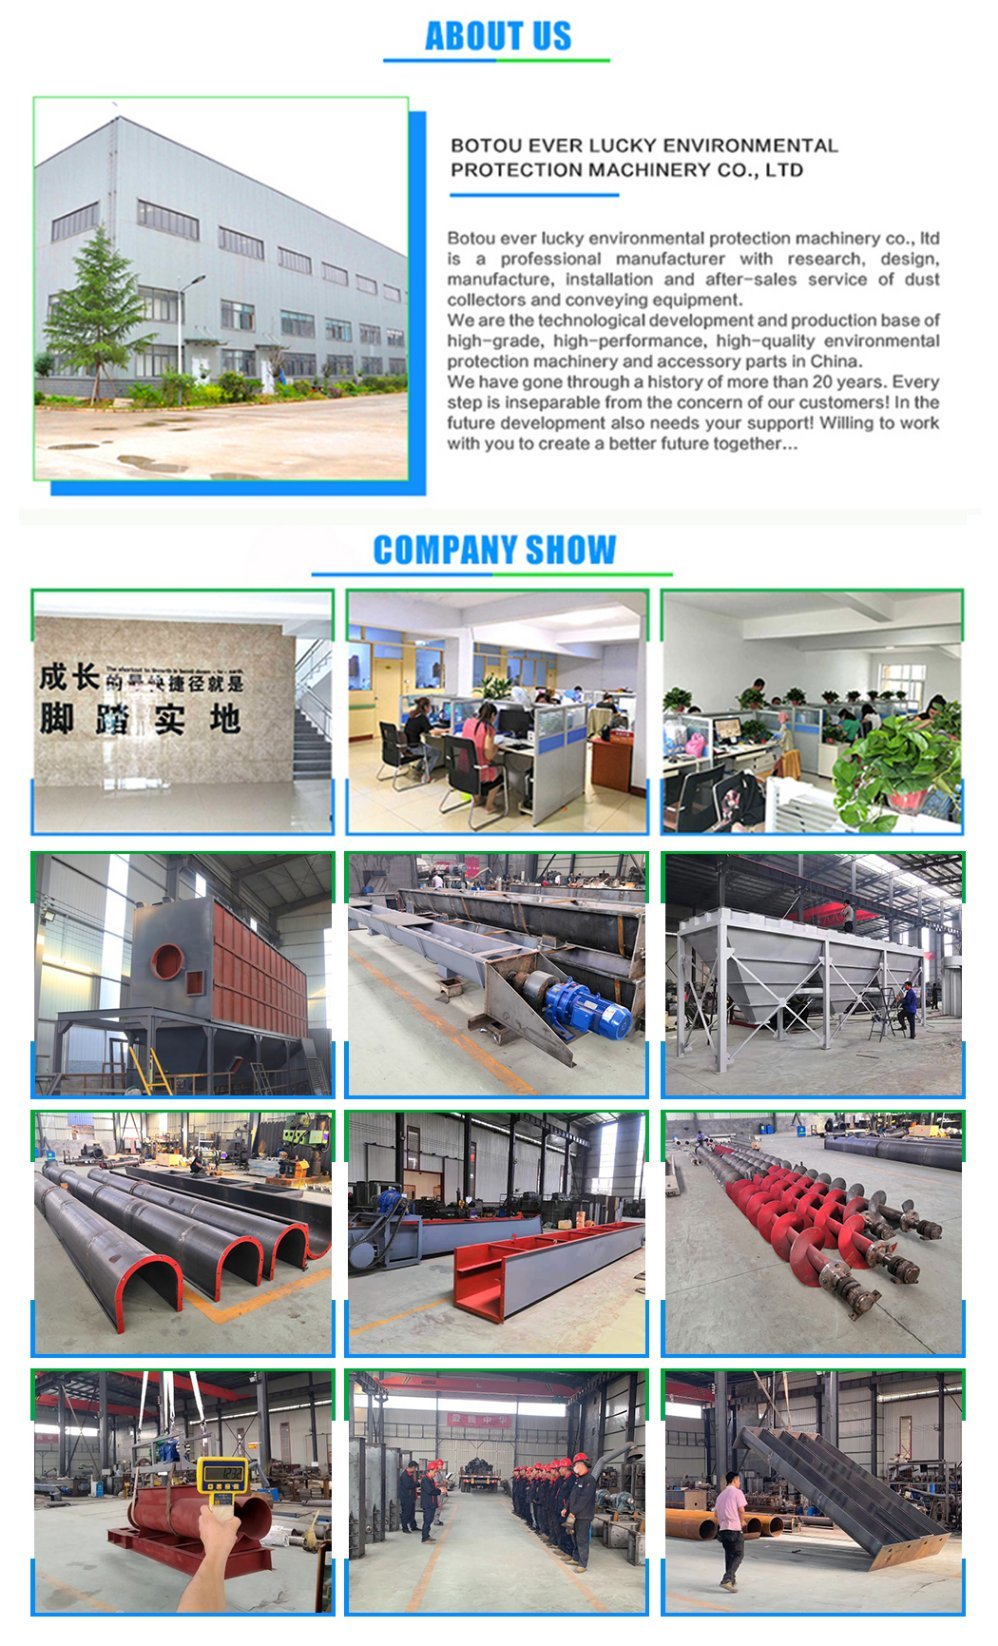
- Stringent Quality Control: Our factory has a comprehensive quality control system in place. Every component of the air slide conveyor system and the diverter valve undergoes rigorous inspection at multiple stages of production. From raw material inspection to final product testing, we ensure that only products that meet our high - quality standards are released.
- Skilled Workforce: Our production team consists of highly skilled and experienced technicians and craftsmen. They are trained in the latest manufacturing techniques and are committed to producing products of the highest quality. Their attention to detail and expertise contribute to the overall reliability and performance of our products.
Keywords
Leave Us A Message
*Note: Please fill in the information accurately and keep the communication open. We will contact you as soon as possible.
Contact Information
Add:Botou city Hebei province
ff0082006
Email us
For more information, please leave your message below.